Manufacturing Defects: One Weld Crack, Four Ways to Classify It
Understand the different types of manufacturing defects, what causes them, and how to prevent them.
- Manufacturing defects can take many forms, from dimensional and material defects to assembly and functional issues.
- Classifying defects by type, origin, severity, and process helps manufacturers understand where and why they occur.
- Early detection, root cause analysis, and process improvements help prevent defects from recurring.
A manufacturing defect is simple to define: a product or component that doesn't meet its required specifications.
Sometimes the problem is obvious: a cracked weld, a dented surface, or a missing component. Other times, it's harder to spot, such as a dimension that's slightly out of tolerance, a material that's out of spec, or a machine that has gradually drifted from its normal operating range.
APQC's benchmark data puts the median manufacturing defect rate at 4,500 defective products per million, or roughly one in every 222 products. The familiar 1–10–100 rule of quality also illustrates how the cost of a problem can increase as it moves further through production and reaches the customer.
The important question, then, isn't simply whether a defect exists. It's understanding what kind of defect it is, where it originated, how serious it is, and how to prevent it from happening again.
Let's break it down.
Types of Manufacturing Defects
Manufacturing defects can take several forms depending on what is wrong with the product. A defect may involve its dimensions, material, surface, assembly, function, or cleanliness.
1. Dimensional Defects
A dimensional defect occurs when a part's size, shape, thickness, or geometry falls outside the specified tolerance.
For example, a machined shaft may be slightly too large to fit its mating component, or a stamped part may have a hole positioned a few millimeters away from its required location.
Common causes include tool wear, incorrect machine settings, calibration issues, and normal process variation.
2. Material Defects
Material defects occur when the raw material doesn't meet the required specifications or contains unwanted properties or contaminants.
Examples include an incorrect material grade, impurities, porosity in castings, or weaknesses in a metal that cause it to fail under load.
These defects may originate with the supplier or develop during processing.
3. Surface Defects
Surface defects affect the appearance or physical condition of a component. Scratches, dents, cracks, burrs, pits, discoloration, and poor coatings are common examples.
Some are primarily cosmetic. Others can affect performance, particularly when a surface crack develops into a larger structural failure.
4. Assembly Defects
Assembly defects occur when components are installed incorrectly, incompletely, or in the wrong sequence.
A missing fastener, incorrect component orientation, loose connection, or improperly torqued bolt can all create an assembly defect. Every individual part may be within specification, yet the finished product can still fail.
5. Functional Defects
A product can look perfectly fine and still fail to do what it was designed to do.
Functional defects occur when a product doesn't perform according to its requirements. An electric motor that doesn't reach its required speed, a valve that fails to open, or a sensor that produces inaccurate readings are examples.
These defects are often difficult to identify through visual inspection alone and may require functional or end-of-line testing.
6. Contamination Defects
Contamination defects occur when foreign material ends up in or on a product where it doesn't belong.
Metal shavings left inside a gearbox, dust on a circuit board, oil residue before painting, or particles in a medicine vial are all examples.
The impact depends on the application. In general manufacturing, contamination may cause wear or poor surface finish. In food, pharmaceuticals, medical devices, and electronics, it can make a product unsafe or unusable.
How Manufacturing Defects Are Classified
The types above describe what is wrong with the product. But manufacturers can look at the same defect in other ways to understand where it came from, how serious it is, and which production process is involved.
These classifications provide different pieces of the same picture.
By Origin
Origin asks where the problem started. A defect may be introduced during manufacturing, originate in the product's design, or occur during packaging and labeling.
This distinction matters because the corrective action depends on the source. A dimensional error caused by a worn machine tool requires a different response from a dimensional requirement that was incorrect in the first place.
By Severity
Severity asks what could happen if the defect is left unresolved. A simple way to assess it is to consider its impact on:
- Safety: Could it cause injury or create a hazardous condition?
- Function: Could it prevent the product from performing as intended?
- Requirements: Does it violate a specification, regulation, or customer requirement?
These impacts are commonly used to distinguish critical, major, and minor defects, although the exact thresholds depend on the industry and applicable quality standards.
By Manufacturing Process
Process-based classification asks which operation is associated with the defect.
Different processes have different failure modes. Casting can produce porosity and shrinkage, welding can produce incomplete fusion and cracks, and injection molding can produce flash, sink marks, and warping.
This classification is particularly useful during troubleshooting because it narrows the investigation to the equipment, parameters, materials, and conditions involved in that operation.
Putting the Classifications Together
These classifications aren't mutually exclusive. A single defect can be described from several perspectives.
Take a crack in a welded component. It could be a surface defect by type, manufacturing-origin by source, critical by severity, and welding-related by process.
Looking at all four perspectives gives a more complete picture of the problem and helps narrow down where to investigate.
Managing and Preventing Manufacturing Defects
Identifying a defect is only the first step. Manufacturers need to detect problems early, determine why they occurred, and change the process so they don't keep coming back.
For a closer look at how these activities fit into a broader quality control system, see our guide to automotive quality control.
Detect Defects Early
The earlier a defect is detected, the easier it is to contain and correct.
Visual inspection and vision systems can identify visible problems, while SPC can reveal unusual variation in measurements. Sensor-based monitoring can track conditions such as temperature, pressure, vibration, and cycle time.
Used together, these methods can help identify not only what went wrong, but also when the process began to change.
That depends on getting machine and sensor data off the shop floor in the first place. FlowFuse connects PLCs, sensors, and inspection systems, so process conditions can be monitored as they happen and a shift in temperature or cycle time shows up before it turns into a batch of rejects.
Find the Root Cause
Detecting a defect tells you what went wrong. Finding the root cause explains why it happened.
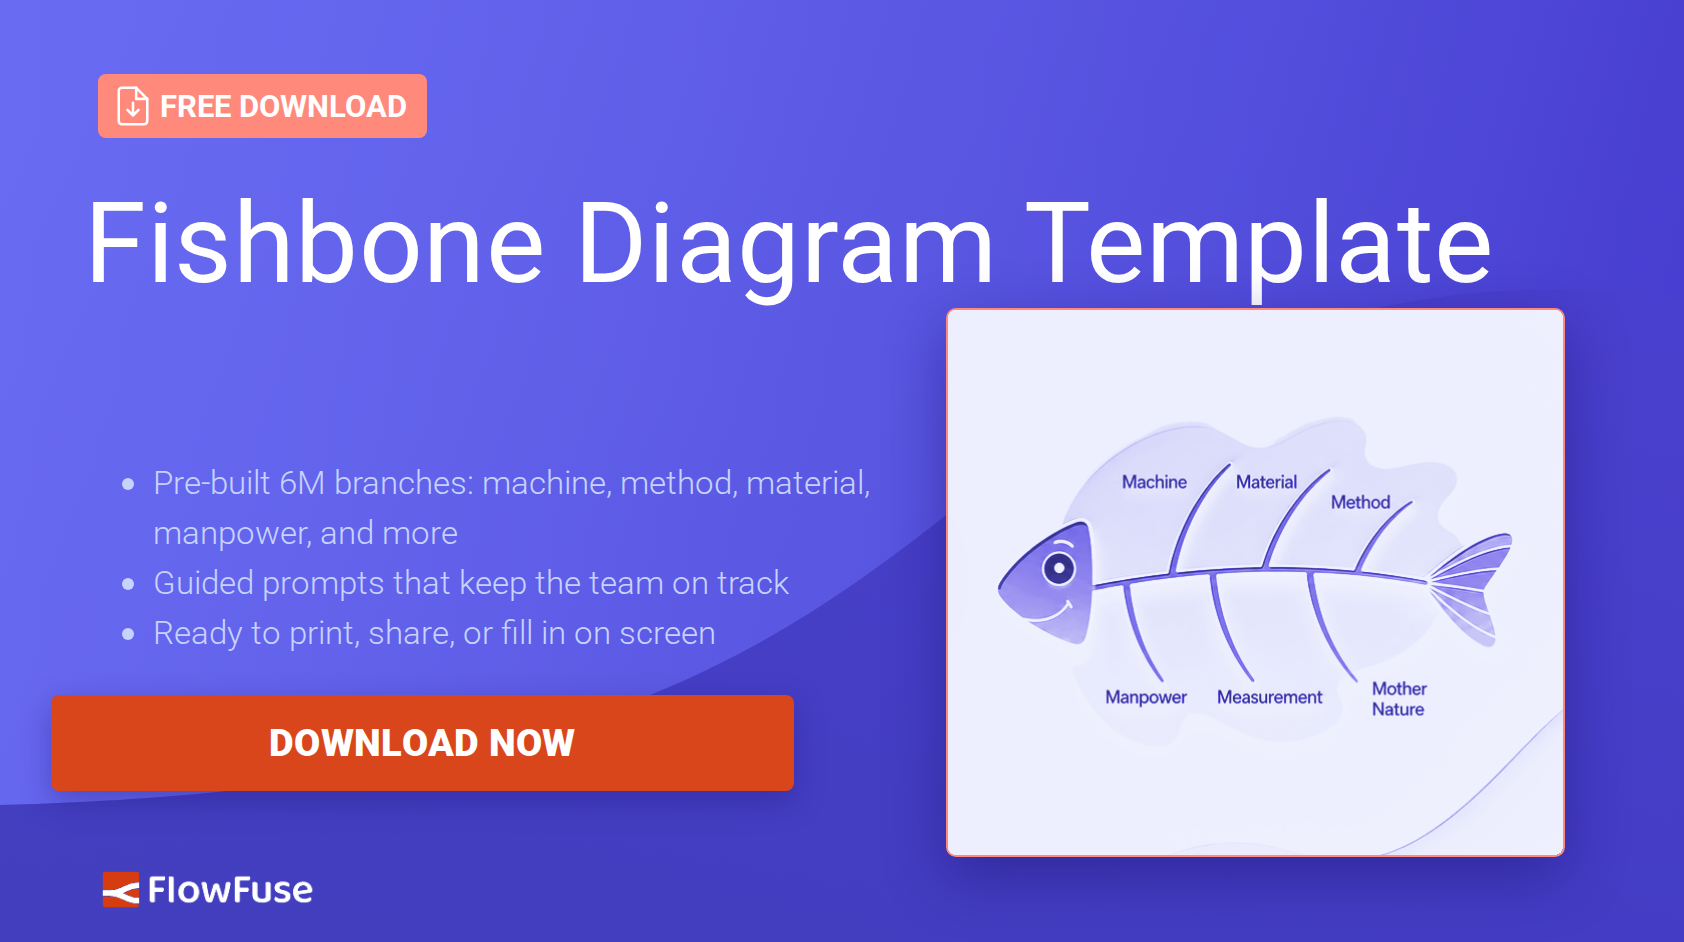
A fishbone diagram helps teams explore possible causes across areas such as machines, materials, methods, measurement, and people. The 5 Whys can then help trace the problem further toward its underlying cause.
The goal is not simply to remove the defective product. It is to identify and address the process condition that produced it.
Prevent Defects From Recurring
Once the cause is understood, manufacturers can modify the process to reduce the chance of the defect returning.
Poka-yoke, or mistake-proofing, can prevent common errors by making them difficult or impossible to introduce. Pareto analysis can help identify which recurring defect types account for the largest share of rejects, allowing teams to focus improvement efforts on the problems occurring most often.
A defect tracking dashboard built in FlowFuse can keep that information visible as new rejects are recorded and help teams monitor whether corrective actions are actually reducing defects over time.
The goal isn't simply to remove defective products from the production line. Each defect is also a signal about the process. When manufacturers understand what went wrong, find its root cause, and act on that information, they can reduce variation and make future production runs more reliable.
Catch the Drift Before It Becomes Scrap
See how FlowFuse connects your machines, sensors, and inspection systems so a shift in temperature, pressure, or cycle time shows up live, before it turns into a batch of rejects.
Frequently Asked Questions
About the Author
Sumit Shinde
Technical Writer
Sumit Shinde is a Technical Writer at FlowFuse specializing in industrial automation and manufacturing. In the past three years, he has built industrial applications and authored more than 100 technical articles covering industrial connectivity, unified data architecture, production metrics, and quality management for modern manufacturing.
Like what you're reading?
Add FlowFuse as a preferred sourceOn the page that opens, check the box next to flowfuse.com to see more of our articles in your Google Search results.
Related Articles:
- Automotive Quality Control 101: Lessons From a 470,000-Vehicle Recall
- Automotive ERP: Integrating with Shop-Floor Systems
- 5 Whys vs. Fishbone Diagram: Which Is Right for You?
- PPAP: How Suppliers Prove a Production Process Is Ready
- 5 Whys Analysis Template: Free Download